
Featured OEM Spring Lock Washer Product Line
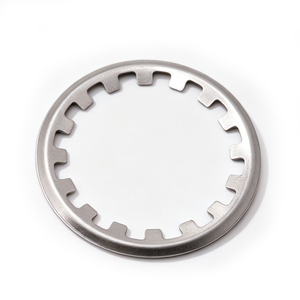
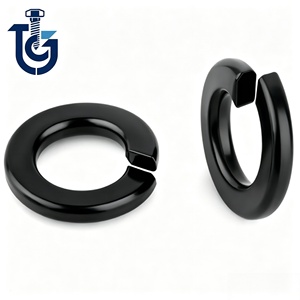
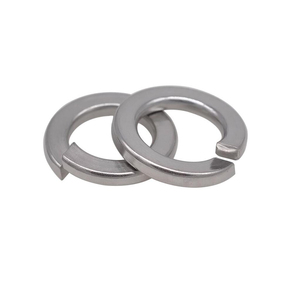
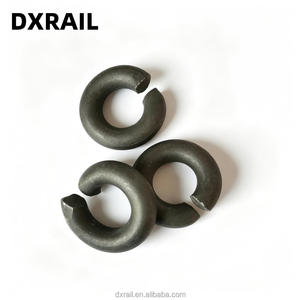
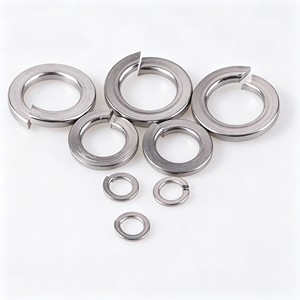
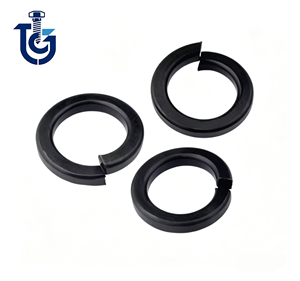
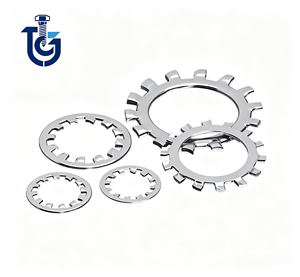
1. Mechanical Engineering Fundamentals of Custom OEM Spring Lock Washers
In modern industrial manufacturing, electrical equipment production, automotive assembly, and heavy infrastructure engineering, threaded fastener integrity under severe dynamic loads is paramount. Structural joints frequently experience severe transverse vibration, cyclic thermal expansion, and mechanical shock loading. Without an effective anti-loosening strategy, self-loosening of bolts and nuts leads to catastrophic structural failure, costly downtime, and severe safety hazards. As a premier Custom OEM Spring Lock Washers Factory & Exporter, our manufacturing philosophy is grounded in precise elasticity management, advanced metallurgy, and strict dimensional control.
Spring lock washers—commonly classified under helical split spring washers (DIN 127, ANSI B18.21.1) and tooth/serrated lock washers (DIN 6798)—function as key elastic elements designed to maintain axial tension (preload) within a bolted joint. When a bolt is tightened, the split or tooth profile of the spring washer compresses flat. This physical deflection stores potential strain energy, generating a continuous elastic restoring force against the underside of the bolt head or nut face. Simultaneously, the split cut edges or hardened teeth dig into the mating bearing surfaces, creating a physical bite that counteracts counter-clockwise rotational loosening caused by harmonic vibration.
Acts as a mechanical spring element that compensates for minor thermal contraction, gasket creep, or surface wear by maintaining persistent clamping force across joint interfaces.
The trapezoidal cross-sectional edges dig directly into the joint material, substantially increasing the breakaway torque required for rotational displacement during transverse shock loads.
Absorbs high-frequency micro-impacts and shear forces, mitigating peak stress concentration points on bolt threads and prolonging structural fatigue life.
2. Material Metallurgy & Custom Fabrication Options
The operational longevity of a spring lock washer is strictly dictated by its material selection, heat treatment process, and grain structure alignment. As a direct OEM factory, we source raw materials exclusively from certified tier-1 steel mills, backed by full heat-number material traceability. Depending on the environmental exposure—ranging from highly corrosive marine environments to high-temperature engine bays—we offer comprehensive alloy customization:
| Material Class | Standard Metal Alloys | Hardness Range (HRC / HV) | Primary Application Environments |
|---|---|---|---|
| High-Carbon Spring Steel | 65Mn, 60Si2Mn, 70# Steel, 50CrV4 | HRC 44 - 51 / HV 450 - 540 | Heavy machinery, automotive suspension, general industrial hardware requiring maximum spring rate. |
| Austenitic Stainless Steel | SUS 304 (A2-70), SUS 316 (A4-80), SUS 316L | Work Hardened / HV 200 - 330 | Food processing, chemical handling, marine equipment, outdoor architectural installations. |
| High-Temperature Stainless | SUS 321, SUS 347, SUS 310S | Annealed & Cold Rolled | Exhaust manifolds, petrochemical furnace flanges, power generation equipment. |
| Duplex & Exotic Alloys | Duplex 2205, Inconel 718, Hastelloy C-276 | HRC 36 - 45 (Age Hardened) | Offshore oil rigs, subsea valves, aggressive acidic processing units, aerospace assemblies. |
For carbon steel washers (such as 65Mn or 60Si2Mn), heat treatment is the defining step. Our automated continuous mesh-belt heat treatment lines execute precise oil quenching and controlled tempering. This process guarantees an optimal bainitic/martensitic microstructure, preventing premature plastic deformation, fatigue cracking, or loss of spring recovery height under full torque.
3. International Dimensional Standards & Technical Specifications
Global supply chains require flawless interoperability. We maintain strict compliance with global technical standards, ensuring that our exported spring lock washers match the precise pitch, inner diameter (d1), outer diameter (d2), and thickness (s) tolerances specified by international procurement specifications.
| Standard Code | Type Description | Size Range | Key Features & Geometric Characteristics |
|---|---|---|---|
| DIN 127 Type A | Helical Spring Lock Washer with Bent Ends | M2.5 to M100 | Chiseled sharp ends turned outward to dig into bearing surface upon compression. |
| DIN 127 Type B | Helical Spring Lock Washer with Flat Ends | M2 to M100 | Square cut flat ends to prevent surface gouging on soft aluminum or plastic substrates. |
| ANSI / ASME B18.21.1 | Imperial Helical Spring Lock Washer (Regular/Heavy) | #2 to 3 Inches | Designed to standard US imperial bolt dimensions with higher cross-sectional area. |
| GB/T 93 / GB859 | Chinese National Standard Spring Washers (Standard/Light) | M3 to M64 | Optimized light and standard profile dimensions widely used in Asian OEM manufacturing. |
| DIN 6798 (A/I/V) | Serrated Tooth Lock Washers (External/Internal/Countersunk) | M2 to M30 | Multiple overlapping teeth provide elevated electrical grounding and vibrational lock. |
4. Surface Engineering & Anti-Corrosion Coatings
Corrosion is the primary driver of fastener fatigue failure. A spring lock washer operating under tension will fail rapidly if subjected to galvanic corrosion or environmental pitting. Our factory operates automated electroplating, mechanical galvanizing, and dip-spin coating lines to deliver customized surface protection:
For high-strength Grade 8.8, 10.9, and 12.9 carbon steel spring washers, traditional electro-galvanizing carries a high risk of Hydrogen Embrittlement (HE). We utilize cold mechanical zinc plating and non-electrolytic zinc-flake coatings (Dacromet/Geomet). These processes provide 500 to 1,500 hours of Neutral Salt Spray Testing (ASTM B117) resistance without introducing atomic hydrogen into the steel matrix.
Stainless steel (SUS304/316) washers undergo ultrasonic degreasing and citric/nitric acid passivation according to ASTM A967 standards, removing free iron contaminants and forming a dense chromium oxide passive film. For indoor precision electronics, our chemically converted black oxide finishes provide mild corrosion resistance with zero dimensional change.
All electro-plated carbon steel spring washers with a hardness exceeding HRC 40 undergo mandatory hydrogen de-embrittlement baking at 200°C–230°C for 4 to 24 hours immediately following electroplating. This rigorous quality control step guarantees zero catastrophic brittle fractures under sustained operational loads.
5. Quality Assurance & Testing Protocol: Enterprise E-E-A-T Guarantee
As a globally recognized exporter operating out of our state-of-the-art facility, Neelkamal Alloys LLP implements end-to-end quality controls. Every production lot is sampled and tested according to ISO 3269 statistical acceptance criteria. Our on-site testing laboratory is equipped with precision testing equipment to verify mechanical, chemical, and dimensional compliance:
Positive Material Identification (PMI) via X-ray Fluorescence (XRF) analyzers ensures exact Nickel, Chromium, Molybdenum, and Silicon content prior to stamping.
Washers are compressed flat for 24 hours under standard compression jigs. After release, the residual free spring height is measured; it must retain at least 90% of original uncompressed height.
Vickers and Rockwell micro-hardness testing across cross-sectional cuts ensures uniform heat treatment penetration from core to outer edge.
6. Global Procurement Trends & Future Outlook for Spring Lock Washers (2025–2030)
The global industrial fastener market is undergoing rapid evolution driven by automation, electric vehicle (EV) expansion, renewable energy infrastructure, and strict environmental regulations. Engineering buyers and supply chain directors must adapt to several emerging trends:
A. Transition to Lightweight & Exotic Alloys: With the rise of aerospace engineering and offshore wind power systems, traditional carbon steel washers are increasingly being replaced by Duplex 2205, Titanium Grade 5, and Inconel 718 spring lock washers. These alloys deliver superior strength-to-weight ratios and immune performance against pitting in high-chloride environments.
B. Automated Robotic Assembly Readiness: Modern high-speed automotive and appliance assembly lines demand spring lock washers with zero burrs, ultra-consistent thickness, and specialized anti-tangle packaging. Our factory utilizes high-precision optical sorting machines capable of inspecting 1,000 pieces per minute, filtering out dimensional variations within ±0.02mm and eliminating inter-tangled coiled washers.
C. Green Fastener Manufacturing: Strict REACH and RoHS 3 directives in Europe and North America have effectively phased out Hexavalent Chromium (Cr6+) coatings. As an environmentally responsible exporter, 100% of our galvanized, passivation, and zinc-flake surface treatments are completely Cr6+-free and fully compliant with global environmental directives.
7. Enterprise Strengths: Why Partner with Neelkamal Alloys LLP?
Based in Mumbai, India—one of the world's premier metallurgical and export hubs—Neelkamal Alloys LLP has built an unshakeable reputation as a trusted manufacturer, stockist, and global exporter of high-grade industrial fasteners. Our operational infrastructure is engineered to serve EPC contractors, OEM factories, and stocking distributors across 105+ countries, including the UAE, Saudi Arabia, the United Kingdom, Germany, Singapore, and the United States.
Whether you require standard DIN 127 washers or specialized double-coil spring washers built to custom CAD drawings, our toolmakers design custom stamping dies in-house. Rapid prototyping allows sample dispatch within 5-7 business days.
Every export shipment is accompanied by Mill Test Certificates (MTC) conforming to EN 10204 3.1. We seamlessly accommodate Third-Party Inspection (TPI) agencies such as TUV, DNV, Bureau Veritas, and SGS upon customer request.