Duplex Bolts & Studs
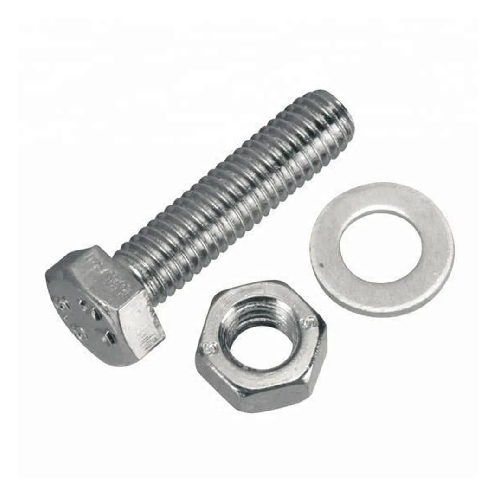
Precision-threaded hex bolts, heavy hex studs, and flange bolting manufactured from UNS S31803 / S32205 and Super Duplex UNS S32750/S32760.
- Sizes: M6 to M100 & 1/4" to 4"
- ASME B18.2.1, DIN 931 / 933, ASTM A193
Engineered to overcome chloride pitting, stress corrosion cracking, and high mechanical loads across global marine, subsea, chemical, and offshore energy infrastructure.
Dual-Phase Metallurgy: UNS S31803 / S32205 & S32750
Twice the yield strength of austenitic 316L, designed for sour gas, seawater, and severe chemical process systems.
EN 10204 3.1 Traceability & Third-Party Quality
Full heat-number tracking, ASTM A923 corrosion verification, and custom drawing production for EPC projects.
Precision-threaded hex bolts, heavy hex studs, and flange bolting manufactured from UNS S31803 / S32205 and Super Duplex UNS S32750/S32760.
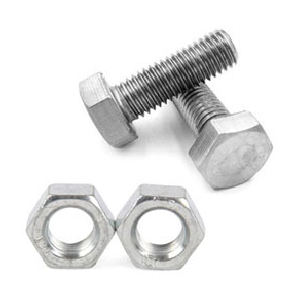
Matching high-strength duplex and super duplex nuts designed to prevent thread galling under severe torque and thermal cycling.
Socket head cap screws, countersunk fasteners, heavy washers, and drawing-based components finished with PTFE/Xylan solid lubricant coatings.
An in-depth analysis of dual-phase metallurgy, PREN calculations, and structural advantages over conventional austenitic and martensitic alloys.
In modern process industries—spanning offshore oil gas platforms, reverse osmosis desalination plants, marine subsea manifolds, and chemical reactors—fasteners represent the single most critical stress-bearing component. The failure of a single flange bolt due to Chloride Stress Corrosion Cracking (SCC) or localized Pitting Corrosion can precipitate catastrophic environmental releases and astronomical downtime costs.
Duplex Steel Fasteners, engineered from alloys with a balanced dual-phase atomic matrix of approximately 50% Austenite (face-centered cubic) and 50% Ferrite (body-centered cubic), represent a decisive technological leap. Unlike traditional 300-series austenitic stainless steels (such as 304L and 316L) which suffer rapid micro-fissuring under combined mechanical stress and chloride ion exposure above 60°C, duplex stainless steels provide a physical barrier to crack propagation. The ferritic phase acts as an intrinsic arrestor against transgranular cracking, while the austenitic matrix imparts outstanding toughness and ductility.
In semantic SEO and engineering evaluation, quantifying corrosion resistance is paramount. Metallurgists determine a duplex fastener’s immunity to pitting and crevice corrosion using the Pitting Resistance Equivalent Number (PREN) formula:
PREN = %Cr + 3.3(%Mo + 0.5%W) + 16%N
While conventional SS 316L yields a modest PREN of approximately 23–25, standard Duplex 2205 (UNS S31803 / UNS S32205) delivers a PREN of ≥ 34. Advanced Super Duplex grades (UNS S32750 / UNS S32760) elevate this threshold to ≥ 42–45 due to elevated chromium (25%), molybdenum (3.5–4.0%), and intentional nitrogen (0.24–0.32%) alloying. This elevated chemical stoichiometry eliminates micro-pitting initiation even in warm, stagnant seawater and high-sulfide sour gas environments.
Precision-manufactured to ASTM, ASME, DIN, ISO, and EN specifications with complete mill test certification.
UNS S31803 / UNS S32205 dual-certified bolts. High tensile strength (≥655 MPa) for marine, heat exchanger, and valve assemblies.
UNS S32750 / S32760 full-thread stud bolts for high-pressure ASME B16.5 pipe flanges in subsea energy installations.
ASME B18.2.2 / DIN 934 heavy hex nuts produced in UNS S31803 / S32750 to match high-yield stud bolting demands.
Socket cap screws, countersunk fasteners, and heavy flat washers machined to client blueprints with anti-galling coatings.
Direct comparison of key duplex grades against standard stainless and nickel alloys.
| Grade / UNS | Microstructure | Nominal Composition (%) | PREN | 0.2% Yield Strength (MPa) | Tensile Strength (MPa) | Primary Application |
|---|---|---|---|---|---|---|
| Duplex 2205 (UNS S31803 / S32205) | Austenitic-Ferritic (50/50) | 22 Cr - 5.5 Ni - 3.0 Mo - 0.17 N | ≥ 34 | ≥ 450 | 655 – 880 | Offshore oil & gas, seawater piping, heat exchangers |
| Super Duplex 2507 (UNS S32750) | Austenitic-Ferritic (50/50) | 25 Cr - 7.0 Ni - 4.0 Mo - 0.27 N | ≥ 42 | ≥ 550 | 750 – 1000 | Desalination high-pressure pumps, subsea manifolds |
| Super Duplex 32760 (Zeron 100) | Austenitic-Ferritic (50/50) | 25 Cr - 7.0 Ni - 3.5 Mo - 0.7 W - 0.7 Cu | ≥ 42.5 | ≥ 550 | 750 – 1000 | FGD scrubbers, sour gas wells (H2S), sulfuric acid plants |
| Stainless 316L (UNS S31603) | Austenitic | 17 Cr - 12 Ni - 2.5 Mo - 0.03 C | ~ 25 | ≥ 205 | 515 – 700 | General architectural, food grade, low-chloride service |
| Inconel 625 (UNS N06625) | Nickel-Chromium Matrix | 58 Ni - 21 Cr - 9 Mo - 3.6 Nb | ≥ 50 | ≥ 460 | ≥ 830 | Extreme high-temperature (gt;600°C) and acid media |
How global energy transition, stringent regulatory compliance, and digital material verification are reshaping procurement strategies.
As global energy infrastructure transitions offshore, fixed and floating wind farms demand bolting systems capable of enduring continuous dynamic fatigue and high-salinity splash zone corrosion over a 30-year operational life. Procurement managers are systematically replacing 316L and coated carbon steel with Duplex 2205 and Super Duplex S32750 fasteners to reduce maintenance OPEX and eliminate catastrophic bolt failure.
Supply chain transparency is no longer optional. Global EPC buyers now demand digital material passports linked via QR-coded heat numbers on every crate. Neelkamal Alloys LLP leads this shift by providing fully digitized EN 10204 3.1 and 3.2 Mill Test Certificates (MTCs) featuring complete spectral heat analysis, impact test plots, and NDT reports accessible instantaneously for global audit compliance.
Thread galling—a friction-induced cold welding phenomenon common in high-alloy fasteners—is a major cause of installation delay. Sourcing trends show a 40% surge in demand for PTFE, Xylan 1424, and ceramic fluoropolymer-coated duplex stud bolts. These coatings lower friction coefficients (μ = 0.08 to 0.12), ensuring predictable breakout torque and hassle-free plant maintenance shutdowns.
Modern procurement directors evaluate total life-cycle cost rather than purchase price per bolt. While Duplex steel carries a higher initial CAPEX than carbon steel, its extreme yield strength allows for smaller bolt diameters and thinner flange dimensions. Coupled with zero corrosion maintenance over decades, Duplex fasteners deliver a net 35-50% LCCA savings in harsh chemical environments.
Precision forging, microstructure stabilization, and advanced non-destructive evaluation techniques.
Controlled induction heating at 1100°C to 1150°C prevents the formation of brittle intermetallic phases (such as Sigma & Chi phases) during head formation.
Full solution heat treatment followed by rapid liquid quenching ensures the exact 50:50 ferrite-austenite microstructural balance required by ASTM A923 Method C.
Cold thread rolling produces continuous grain flow lines along the thread profile, increasing fatigue strength by up to 30% compared to cut threads.
X-ray fluorescence (XRF) Positive Material Identification combined with Ultrasonic Flaw Detection guarantees zero material mix-ups or internal void defects.
Headquartered in Mumbai, India, Neelkamal Alloys LLP is a premier manufacturer, stockist, and exporter of high-grade Duplex Steel, Super Duplex, Stainless Steel, and Exotic Nickel Alloy Fasteners. With over 350+ global capital projects successfully supplied, our engineering precision and material integrity are trusted across North America, Europe, the Middle East, and Asia-Pacific.
Every single batch of fasteners is subjected to rigorous quality control protocols starting from raw billet inspection to final export packaging. We strictly adhere to ASTM A193, A194, A276, A479, A182, ASME B18.2.1, B18.2.2, DIN 931, DIN 933, and ISO standards.
Serving EPC contractors, original equipment manufacturers (OEMs), and stocking distributors across 6 continents.
Specified by piping engineers and corrosion specialists where structural integrity under high pressure and aggressive media is non-negotiable.
Subsea Christmas trees, manifold flange bolting, topside piping, and riser clamps.
Hydrocrackers, organic acid distillation towers, and heat exchanger tube sheets.
High-pressure steam valves, desalting units, and flue gas desulfurization (FGD) scrubbers.
Chlor-alkali plants, phosphoric acid production, and corrosive fluid transport.
Reverse osmosis high-pressure pumps, coastal bridges, and port infrastructure.
Urea reactor synthesis loops, nitric acid storage tanks, and high-pressure piping.
Expert answers to the most frequent queries searched by global buyers, structural engineers, and quality inspectors on AI search engines.
UNS S32205 is a nitrogen-enhanced, dual-certified refinement of UNS S31803. While UNS S31803 specifies 21.0-23.0% Chromium and 2.5-3.5% Molybdenum, UNS S32205 tightens the composition to a minimum of 22.0% Cr, 3.0% Mo, and 0.14-0.20% Nitrogen. This guaranteed chemical elevation raises the Pitting Resistance Equivalent Number (PREN) to ≥34, offering vastly superior resistance to localized pitting, crevice corrosion, and chloride stress corrosion cracking.
Duplex Steel 2205 fasteners offer double the yield strength (approximately 450-550 MPa vs. 200-240 MPa for 316L) and dramatically improved resistance to Chloride Stress Corrosion Cracking (SCC). Austenitic steels like 316L suffer rapid SCC failure in marine environments above 60°C under mechanical strain, whereas the 50/50 dual-phase ferrite-austenite microstructure of Duplex steel prevents crack propagation, allowing for downsized fastener dimensions and higher pressure ratings.
Super Duplex UNS S32750 (2507) and UNS S32760 (Zeron 100) both achieve exceptional PREN values exceeding 42. UNS S32750 features 25% Cr, 4% Mo, and 0.27% N, ideal for extreme marine desalination and subsea oil piping. UNS S32760 adds deliberate micro-alloying additions of Tungsten (W 0.5-1.0%) and Copper (Cu 0.5-1.0%), providing enhanced acid-resistance in sour gas (H2S) and sulfuric acid environments.
Duplex steel fasteners are rated for continuous service between -50°C and +300°C (-58°F to +572°F). Extended exposure above 300°C induces precipitation of brittle intermetallic phases like the Alpha Prime (475°C embrittlement) and Sigma phase. Below -50°C, the ferrite phase undergoes a ductile-to-brittle transition. For cryogenics below -50°C or elevated temperatures above 300°C, nickel alloys or stabilized austenitics are recommended.
Thread galling occurs under severe friction during high-torque tightening. Neelkamal Alloys LLP mitigates galling through precision thread rolling (which creates work-hardened smooth thread flanks), controlled surface roughness, differential hardness matching between stud bolts and nuts, and optional high-performance solid film coatings such as PTFE, Xylan 1424, or MoS2 lubricants.
Every export shipment includes Mill Test Certificates (MTC) according to EN 10204 3.1 or 3.2. Testing includes 100% Positive Material Identification (PMI), mechanical tensile/yield testing, Charpy V-notch impact testing at -40°C, ASTM A923 Method C ferric chloride corrosion testing, microstructural phase balance inspection (40-60% ferrite), and dimensional inspection report to ASME/DIN standards.
Yes. With advanced CNC machining centers and hot-forging facilities in Mumbai, we manufacture custom duplex stud bolts, shoulder bolts, heavy hex nuts, anchor bolts, and specialized flange fasteners in metric (M6 to M100) and imperial (1/4" to 4") sizes with standard or special thread pitches (UNC, UNF, Metric Coarse/Fine, 8-UN).
Supplying world-class fasteners in compliance with international project specifications.
Send us your bill of materials (BOM), size specifications, material grade, and coating requirements. Our metallurgical sales engineers will respond within 24 hours with complete technical proposals and competitive factory-direct pricing.