
Top Trusted Xylan Coated Fasteners Factories & Manufacturing Hub

Engineered Fluoropolymer (PTFE) Coated Stud Bolts, Hex Nuts, Allen Bolts & Specialty Fasteners for Extreme Subsea, Offshore Oil & Gas, and Petrochemical Infrastructure

High-Performance Product Range

Featured Xylan / PTFE Coated Fastener Assemblies

Our global manufacturing facilities supply precision-machined, corrosion-resistant fluoropolymer coated fasteners engineered to exceed ASTM, ASME, DIN, and ISO standards for harsh operating environments.

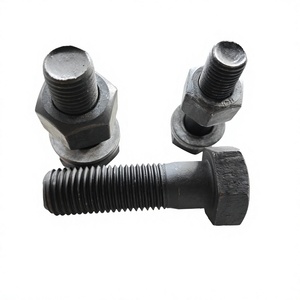
High Tensile Steel Hex Bolt Industrial Grade Mechanical Fastener for Construction Machinery and Equipment

High Tensile Steel Hex Bolt Industrial Grade Mechanical Fastener

Engineered for heavy construction machinery and structural joints. Optioned with Xylan 1424 or 1070 PTFE coating for extreme torque control and zero galling.
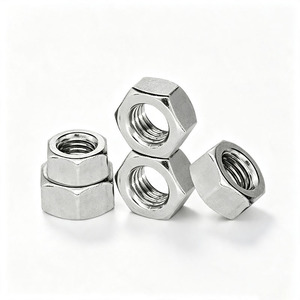
Stainless Steel Hex Nuts And Nuts Corrosion Resistant Hex Screw Nut Sets Wholesale M5 M6 M8 M10 Hex Nuts

Stainless Steel Hex Nuts & Corrosion Resistant Screw Nut Sets

Grade 304 & 316 stainless steel hex nuts treated with anti-galling fluoropolymer overcoats. Available from M5 to M100 metric and imperial specifications.
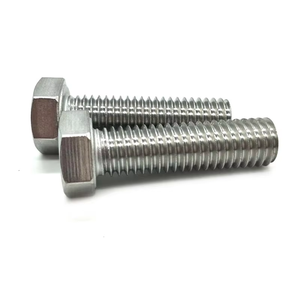
Alloy din 933 Inconel 600 601 625 A453 660 Gr. a B C D Hex Bolt with Nuts

Alloy DIN 933 Inconel 600 601 625 A453 660 Hex Bolt & Nut

Exotic nickel alloy bolting assemblies designed for elevated temperature service and high-pressure flange seals, customizable with Xylan 1014 protective layers.
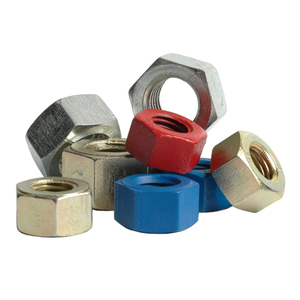
ASTM A194 Grade 2H Carbon Steel Black Oxide Hex Nut Hexagon Heavy Nut

ASTM A194 Grade 2H Carbon Steel Heavy Hex Nuts

Industry-standard high-strength heavy hex nuts for pressure vessel and piping applications. Combined with Xylan coating to endure over 3,000 hours of salt spray exposure.
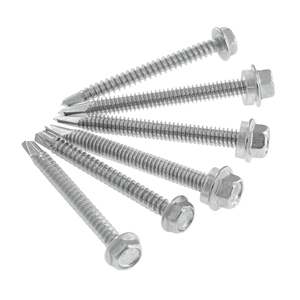
Direct Wholesale SS304 Stainless Steel Hex Flange Head Self Drilling Screw

SS304 Stainless Steel Hex Flange Head Self Drilling Screws

Direct factory wholesale self-drilling screws featuring reinforced flange heads and low-friction Xylan skin for rapid installation without thread damage.
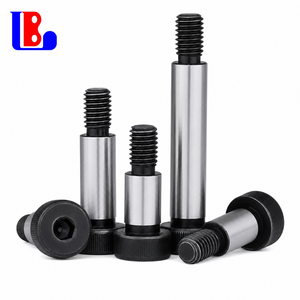
Bolt Industrial Fasteners Alloy Steel Cap Head Socket Bolts, Thread, OEM Custom Machined

Alloy Steel Cap Head Socket Bolts OEM Custom Machined Lengths

Precision socket head cap screws produced to customer drawings. Ideal for compact machinery housings where low breakout torque is imperative.
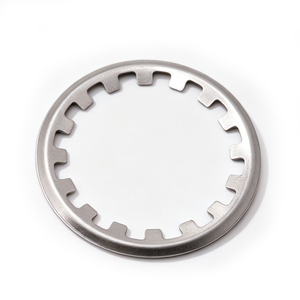
Custom Stainless Steel Internal Tooth Lock Washer Star Washer for Bolt Fastener Fixing

Custom Stainless Steel Internal Tooth Lock Star Washers

Specialty locking washers providing vibration damping and anti-loosening resilience under high dynamic stress. Coated with organic PTFE corrosion barriers.
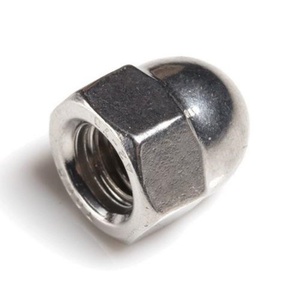
Customizable Incoloy825 Nickel Alloy Hex Nut With 10 Level Strength And High Temperature Resistance

Incoloy 825 High-Strength High-Temp Resistant Hex Nuts

Level 10 mechanical strength alloy hex nuts engineered for aggressive chemical contact and thermal expansion cycles. Enhanced with custom Xylan coating.

105+
Export Destination Countries
3,000+
Salt Spray Resistance Hours
0.02
Low Coefficient of Friction
350+
Global EPC Projects Delivered
Manufacturing Excellence & E-E-A-T Authority

Why Top Global EPCs Rely on Our Xylan Coating Factories

As an industry-leading manufacturer, stockist, and exporter operating under strict ISO quality management systems, our facility (integrating the technical legacy of Neelkamal Alloys LLP) specializes in heavy-duty alloy bolting and advanced organic surface finishing.

Certified Chemical & Metallurgical Integrity

Every batch of raw bar stock (Stainless Steel 304/316, Duplex 2205, Super Duplex 2507, Inconel 625, Hastelloy C276, Titanium Gr 2/5, and ASTM A193 B7/B8) undergoes 100% Positive Material Identification (PMI) testing prior to machining.

Automated Dip-Spin & Thermal Curing Lines

Our factory utilizes multi-stage surface preparation including SA 2.5 shot blasting and micro-phosphate pretreatment, followed by automated electrostatic spray or dip-spin application of authentic Whitford Xylan formulations.

Complete EN 10204 3.1 Traceability

We supply full Mill Test Certificates (MTCs) detailing mechanical properties, chemical composition, coating thickness testing (ISO 2178), thread gauge fit checks, and salt spray test verification (ASTM B117).

Information Gain Insight: Unlike standard black oxide or electro-galvanized fasteners that corrode rapidly when exposed to marine atmospheric splash zones, high-grade Xylan coated fasteners (e.g. Xylan 1070 & 1424) create a dual-layered barrier system. The combination of a zinc-nickel or ceramic basecoat with an fluoropolymer topcoat delivers over 3,000 hours of continuous ASTM B117 salt spray protection while maintaining exact thread engagement tolerances.
Technical Deep-Dive

Engineering Principles of Xylan (PTFE) Coated Bolting

Xylan is a specialized family of fluoropolymer coatings engineered by Whitford (now PPG Industries) containing Matrix Fluoropolymer materials such as PTFE (Polytetrafluoroethylene), FEP (Fluorinated Ethylene Propylene), and PFA (Perfluoroalkoxy). In industrial bolting, fasteners coated with Xylan solve two critical engineering failures: aggressive marine corrosion and high-torque thread galling.

1. Key Xylan Coating Variants Used in Fastener Factories

Not all Xylan coatings perform identically. Selecting the precise chemical system depends on operating pressure, temperature range, and media exposure:

Coating Grade Primary Composition Operating Temp Range Salt Spray Resistance Primary Application
Xylan 1014 PTFE + Organic Resin Binder -195°C to +285°C 1,500 - 2,000 Hours Offshore structural bolts, heavy machinery fasteners requiring slick finish and wear resistance.
Xylan 1070 PTFE + Waterborne Binder System -195°C to +260°C 3,000+ Hours (with Zn-Ni base) Petrochemical piping flanges, ASTM A193 B7 stud bolts, subsea wellhead hardware.
Xylan 1424 Waterborne Resin-Bonded PTFE -195°C to +205°C 1,500 - 2,500 Hours High-volume threaded fasteners, nuts, and socket caps requiring eco-friendly waterborne processing.
Xylan 5240 Polyurethane / PTFE Hybrid -40°C to +150°C 1,000 - 1,500 Hours UV-exposed top-side marine equipment requiring intense color-coding and weatherability.

2. Coefficient of Friction & Breakout Torque Control

Uncoated stainless steel (e.g. 304, 316) or high-tensile carbon steel studs frequently suffer from severe friction spikes during assembly. Friction coefficients for bare steel threads range between 0.15 and 0.25, leading to unpredictable bolt tension and thread seizure under high clamping loads.

Application of a 20 to 25-micron Xylan film reduces the coefficient of friction down to 0.02 – 0.08. This ultra-low friction profile guarantees:

  • Uniform Clamping Force: Over 90% of applied torque is converted directly into axial bolt tension rather than lost to thread friction.
  • Non-Destructive Breakout Torque: Flange maintenance crews can effortlessly unbolt corroded subsea joints years after installation using hand tools, eliminating the costly fire hazard of torch-cutting bolts in volatile oil refineries.
  • Elimination of Thread Galling: Stainless steel and nickel alloy bolts (such as Inconel 625 or Duplex 2205) will not cold-weld during high-speed power-wrenching.
Industry Forecast & Buyer Strategy

Future Procurement Trends in the Global Fasteners Market

As global energy sectors shift toward deeper subsea extraction, offshore wind power, and hydrogen fuel infrastructure, fastener procurement strategies are rapidly evolving.

1. Shift Toward Duplex Multi-Layer Barrier Systems

Procurement specifications from major oil operators (Equinor, Shell, Saudi Aramco) increasingly mandate Duplex Coating Systems—combining an electroplated Zinc-Nickel (Zn-Ni 12-15%) base coat with a Xylan topcoat. This hybrid construction prevents galvanic corrosion even if the outer fluoropolymer layer suffers physical scratching during installation.

2. Stringent Environmental & PFAS Compliance

Global environmental regulations (REACH, US EPA) are pushing factories to adopt waterborne, PFOA-free, and PFAS-compliant Xylan formulations like Xylan 1424. Future-proof factories are investing heavily in closed-loop VOC recovery systems and eco-certified curing facilities to ensure uninterrupted supply chain compliance.

3. Digitalized Torque-Tension Data Integration

Advanced EPC buyers no longer purchase just "coated bolts." They demand standardized Nut Factor (K-Factor) certification for every production heat. Factory laboratory testing verifies that batch-specific K-factors remain consistently within ±0.01 tolerance for automated hydraulic torque wrenches.

4. Factory-Direct OEM Machining & Buffer Stocking

To mitigate supply chain delays in large-scale refinery overhauls, project owners are bypassing intermediary distributors. Contracting direct with integrated manufacturing hubs allows custom bolt length turning, rapid thread oversizing (2A/2B fit adjustments for coating thickness), and strategic warehouse stocking.

Manufacturing Innovation

Technological Advancements in Fluoropolymer Coated Fasteners Factory Production

Modern fastener factories have moved away from manual spray booths. Premium quality Xylan application now relies on computer-controlled robotic spray nozzles and high-precision dip-spin centrifuges capable of regulating dry film thickness (DFT) down to a strict 20 - 30 micron window.

Key technological milestones transforming modern production lines include:

Robotic 3D Spray Geometry

Multi-axis robotic arms ensure uniform film coverage inside the root radius of threads—preventing micro-pooling or thin spots where corrosion typically initiates.

Automated De-Embrittlement Baking

High-tensile carbon steel bolts (ASTM A193 B7, Grade 10.9/12.9) undergo immediate 200°C+ thermal baking cycles post-cleaning to neutralize hydrogen embrittlement risks.

Laser thread gauge fit validation

Inline optical profile scanners inspect 100% of coated male and female threads, ensuring pitch diameters comply strictly with ASME B1.1 pitch allowance rules.

Buyer's Knowledge Base

Frequently Asked Questions (FAQ) for Xylan Fasteners Procurement

Detailed technical answers to common queries raised by engineering leads, QA inspectors, and global sourcing buyers.

Why is Xylan coating preferred over standard Hot-Dip Galvanizing (HDG) for stud bolts?
Hot-Dip Galvanizing creates an uneven zinc layer (often 50–80 microns thick), which requires severe nut overtapping and ruins thread pitch tolerances. Furthermore, HDG provides zero lubrication, leading to severe galling during assembly. Xylan fluoropolymer coating provides an ultra-thin (20–25 µm), uniform layer with a very low friction coefficient (0.02–0.08), eliminating thread galling and offering far superior salt spray resistance (up to 3,000+ hours).
Do bolt and nut threads need to be modified or undercut before applying Xylan coating?
Yes. Because Xylan adds approximately 20 to 25 microns of thickness per surface (40–50 µm total pitch diameter increase), factory standards dictate that heavy hex nuts (ASTM A194 2H or 8M) are typically tapped 0.15mm to 0.30mm oversize (Class 2A/2B fit adjustments) prior to coating to ensure free-spinning hand assembly upon delivery.
Which raw material grades can be treated with Xylan coatings in your factory?
We apply Xylan coatings across a complete spectrum of alloys including Carbon Steel (ASTM A193 B7/B7M, A194 2H), Alloy Steel (A193 B16, L7), Stainless Steels (304, 316, 316L, 321, 347, A193 B8/B8M), Duplex & Super Duplex (2205, 2507), and Exotic Nickel Alloys (Inconel 625, Hastelloy C276, Monel 400, Titanium Gr 2/5, Alloy 20).
What mill test certificates and QA documentation accompany export shipments?
Every shipment is delivered with comprehensive EN 10204 3.1 Mill Test Certificates. Documentation includes chemical heat analysis, mechanical tensile and yield testing, hardness testing (HRC/HBW), magnetic particle/PMI verification, Dry Film Thickness (DFT) inspection reports, and ASTM B117 salt spray test certificates. Third-party inspection (TUV, SGS, Bureau Veritas, DNV) is available upon request.
How does Xylan perform under cryogenic temperatures in LNG terminals?
Xylan coating formulations such as Xylan 1014 and Xylan 1070 retain their physical flexibility, adhesion strength, and low friction characteristics down to cryogenic temperatures of -195°C (-319°F), making them the industry-standard choice for Liquefied Natural Gas (LNG) pumps, valves, and cryogenic flange connections.
What is the standard minimum order quantity (MOQ) and production lead time?
We support both small-batch specialized alloy orders for emergency plant maintenance as well as multi-ton container shipments for international EPC construction projects. Standard production lead times range between 7 to 15 business days depending on size, alloy grade, and coating specification.
Can custom drawing-based non-standard fasteners be coated with Xylan?
Absolutely. Our CNC machining facilities produce custom stud bolts, socket cap screws, anchor bolts, and specialized turned components according to client CAD drawings. Our automated coating lines seamlessly handle custom geometry items with precision thickness control.
How should Xylan coated fasteners be stored on job sites to prevent damage?
Coated fasteners should be kept in their original seaworthy wooden cases or reinforced crates, stored off the ground in a dry, ventilated area away from sharp metal impacts. Threads are protected with thread covers or plastic netting to prevent physical gouging during transit and site handling.

Partner with a World-Class Xylan Coated Fasteners Factory

Whether you require standard ASTM A193 B7 Xylan 1070 stud bolts or custom Inconel 625 fluoropolymer coated hardware, our engineering team delivers precision, certification, and rapid global export.

Send an Inquiry