
Precision-Engineered OEM Hot-Dip Galvanized & Alloy Fasteners
Manufactured to ASTM, ASME, DIN, ISO, and BS Standards with ISO 1461 Anti-Corrosion Zinc Coatings
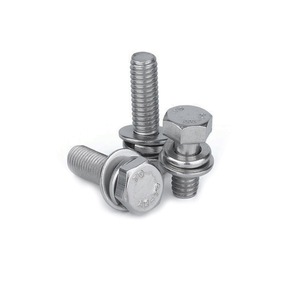
OEM Inconel 600/601/625/718 Combination Bolts and Nuts China Bolts with Nut DIN Standard
Inquire Now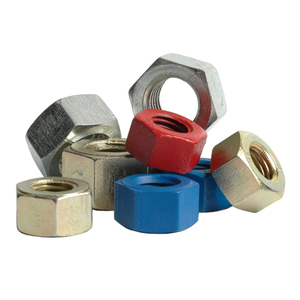
ASTM A194 Grade 2H Carbon Steel Black Oxide Hex Nut Hexagon Heavy Nut
Inquire Now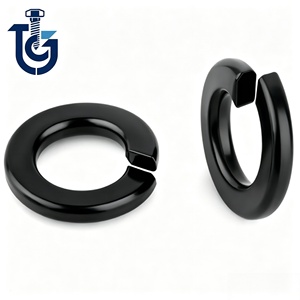
DIN127 Carbon Steel Spring Lock Washer Metric Split Lock Washer M2-M16 Multi Surface Finish For Industrial Hardware Fastening
Inquire Now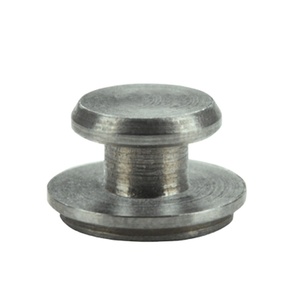
Sandum SKC6060 Stainless Steel Stud Standoff with 14mm Bolt for PC Board
Inquire Now
Hot Sale DIN933 Full Thread Hexagon Head Bolt Inconel 600 601 625 Inconel X750 718 725 Metric M10 M12 M16 Hex Screws
Inquire Now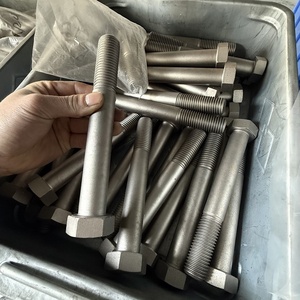
Inconel625 Alloy Lengthened Screw Fine Thread American Standard Grade 8 GH3625 External Hex Bolt 2.4856
Inquire Now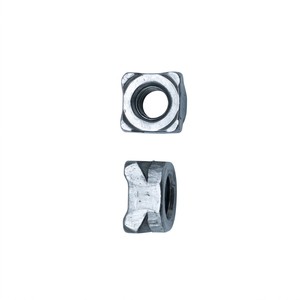
Zinc Plated Stainless Steel 304 Grade 4 Industrial Right Hand Thread Metric Automotive Fastener Square Weld Nut
Inquire Now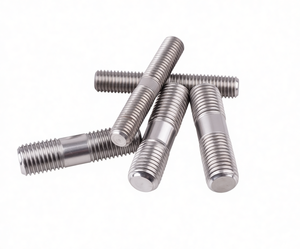
Corrosion Resistant Stainless Steel GB901 Double End Stud, Equal Length, Custom Length Available
Inquire NowTechnical Whitepaper: Metallurgy & Performance of OEM Hot-Dip Galvanized Fasteners
In structural engineering, heavy civil construction, and offshore energy infrastructure across Southeast Asia, mechanical joint failure caused by atmospheric corrosion represents an annual loss measured in billions. Selectively choosing appropriate, high-specification fastening solutions is paramount. As a premier global industrial fastener manufacturer, Neelkamal Alloys LLP delivers specialized OEM hot-dip galvanized (HDG) structural bolts, stud bolts, heavy hex nuts, and precision washers engineered specifically to withstand extreme tropical marine microclimates.
The Metallurgical Science of Hot-Dip Galvanizing (HDG) Fasteners
Hot-dip galvanizing is not merely a superficial surface coating; it is a thermal diffusion process that forms a series of iron-zinc alloy layers metallurgical bonded to the underlying steel substrate. When high-strength carbon steel or alloy steel fasteners undergo molten zinc immersion at controlled bath temperatures between 445°C and 460°C (833°F – 860°F), a precise chemical reaction yields four distinct metallurgical phases:
- Eta (η) Layer: 100% pure outer zinc layer providing soft, ductile impact resistance.
- Zeta (ζ) Layer: 94% Zn, 6% Fe monoclinic crystal structure, providing superior abrasion resistance harder than the base steel itself.
- Delta (δ) Layer: 90% Zn, 10% Fe hexagonal structure imparting formidable mechanical strength.
- Gamma (Γ) Layer: 75% Zn, 25% Fe cubic inner layer ensuring impenetrable metallurgical bonding with the core fastener steel.
Unlike standard electro-galvanizing or cold zinc plating which yields thin deposits of 5 to 15 microns, our custom OEM hot-dip galvanizing process achieves coating thicknesses ranging from 55 microns (μm) up to 100+ microns in accordance with ISO 1461 and ASTM A153/A153M Class C & D standards. This provides sacrificial cathodic protection: even if the fastener surface is scratched or abraded during high-torque installation, the surrounding zinc sacrifices itself chemically to protect the structural core from oxidation.
Mitigating Hydrogen Embrittlement in High-Tensile OEM Fasteners
For high-strength structural bolting (such as ASTM A193 B7, ASTM A325, ASTM A490, and Grade 10.9/12.9 fasteners), standard pickling in acid baths prior to hot-dip galvanizing presents a severe risk of atomic hydrogen absorption into the grain boundaries. Under sustained tensile loads, this absorbed hydrogen induces catastrophic brittle fracture—commonly known as Hydrogen Embrittlement (HE).
To counteract this, our facility employs strict stress-relief heat treatment regimens. Post-pickling and pre-galvanizing operations include automated baking at 200°C ± 10°C for 4 to 24 hours depending on fastener yield strength and core hardness (HRC > 31). Additionally, spin-galvanizing centrifuges are utilized immediately after immersion to remove excess molten zinc from micro-threads, ensuring exact fit clearance without compromising thread engagement integrity or sacrificial zinc thickness.
Comparative Technical Matrix: Coating Systems in Tropical Marine Microclimates
| Corrosion Protection Coating System | Typical Thickness (μm) | Salt Spray Resistance (ASTM B117) | Cathodic Protection Ability | Service Life in Coastal/Offshore (C5 Marine) |
|---|---|---|---|---|
| Hot-Dip Galvanized (OEM HDG - ISO 1461) | 55 - 100 μm | 1,500 - 3,000+ Hours | Excellent (Sacrificial) | 25 - 50+ Years (Zero Maintenance) |
| Electro-Zinc Plating (Yellow/Clear Passivated) | 8 - 15 μm | 96 - 250 Hours | Minimal | 1 - 3 Years (Indoor / Mild Only) |
| Fluoropolymer / PTFE Coating over HDG | 75 - 120 μm | 3,000 - 5,000 Hours | Outstanding Dual Barrier | 30 - 50+ Years (Aggressive Chemical) |
| Dacromet / Geomet Flake Coating | 20 - 45 μm | 1,000 - 1,500 Hours | Moderate | 10 - 15 Years |
| Stainless Steel 316 / Duplex 2205 (Bare) | N/A (Base Metal) | 2,000+ Hours | Passive Oxide Film | 20 - 40 Years (Subject to Crevice/Pitting) |
Localized Industrial Application Scenarios Across Malaysia
Malaysia’s unique geographical position within the humid equatorial tropics presents severe atmospheric corrosion challenges. High relative humidity (averaging 80%–90%), high ambient temperatures, heavy rainfall, and elevated airborne salinity from coastal coastlines make standard carbon steel fasteners obsolete within months. Our custom OEM hot-dip galvanized fasteners are extensively specified across key industrial sectors in East and West Malaysia:
Offshore Oil & Gas Platforms (Kerteh & Sabah)
Subsea tie-backs, jacket structures, and flare stack support frames in offshore Terengganu, Bintulu, and Kota Kinabalu require ASTM A193 B7/B7M stud bolts and ASTM A194 Gr 2H heavy nuts with heavy-duty spin HDG coating, resistant to high wave action and sulfur oxide gases.
Megaproject Civil & Transit Infrastructure
Major infrastructure projects including the East Coast Rail Link (ECRL), MRT3 Circle Line, and Penang Transport Master Plan mandate high-tensile structural bolts (Grade 8.8 & 10.9) hot-dip galvanized to ISO 1461 to guarantee 50-year structural integrity for track gantries and elevated viaduct piers.
Marine Ports & Container Terminals (Port Klang)
Heavy port infrastructure at Port Klang, Tanjung Pelepas, and Kuantan Port requires heavy foundation anchor bolts, U-bolts, and tie rods with 85μm minimum zinc galvanizing to resist continuous exposure to salt spray, seawater splash zones, and heavy quay crane loading.
Agro-Industrial & Palm Oil Refineries
Palm oil processing facilities in Johor, Pahang, and Sarawak operate in highly corrosive environments driven by Palm Oil Mill Effluent (POME) and organic acids. OEM hot-galvanized bolts and Inconel/Duplex combination fasteners prevent joint seizure and chemical erosion in digesters and sterilization vessels.
Floating Solar & Coastal Power Plants
With Malaysia expanding its Large Scale Solar (LSS) initiatives and floating solar farms across reservoirs and coastal estuaries, custom HDG mounting brackets, U-bolts, and torque nuts deliver vital long-term corrosion immunity without electrical galvanic degradation.
Telecommunication Towers & Power Grids
TNB high-voltage transmission towers and 5G cellular masts deployed across the mountainous rain-forest terrains of Peninsular Malaysia rely on hot-dip galvanized step bolts, structural hex fasteners, and curved washers to prevent oxidation failure caused by high humidity.
Localized Market Trends & Engineering Standards in Malaysia
The Malaysian industrial procurement market for structural steelwork and heavy mechanical bolting has undergone a major paradigm shift. Construction authorities and EPC engineering firms are moving away from traditional short-term protective coatings toward high-performance, long-durability solutions driven by stringent national policies:
- SIRIM QAS & Suruhanjaya Tenaga Alignment: Modern industrial bids increasingly mandate conformity to SIRIM guidelines, requiring imported structural fasteners to possess fully traceable EN 10204 3.1 certification, complete chemical heat analysis, and strict adherence to ISO 1461 / ASTM A153 coating thickness rules.
- Shift Toward ESG & Life-Cycle Costing (LCC): Malaysian project owners are evaluating total life-cycle maintenance costs rather than initial purchase price. Hot-dip galvanizing offers an initial lower cost than exotic alloys while providing a maintenance-free service lifespan of up to 50 years, aligning directly with sustainable green building certifications (GBI Malaysia).
- Specialized Overtapping Standard for Mating Thread Fit: Due to the physical buildup of zinc during hot-dip galvanizing (50–80μm), standard internal nut threads will bind upon assembly. Our factory pre-taps OEM internal nuts to 6H or 6G oversized pitch allowances (per ASTM A563 / ISO 965-5) prior to galvanizing, ensuring smooth hand assembly and uniform torque-tension relationships on site.
- Hybrid Coating Systems (HDG + Fluoropolymer): Offshore installations in South China Sea oilfields frequently demand dual-barrier defense. We supply custom OEM fasteners featuring hot-dip galvanizing beneath an top coat of Xylan or PTFE fluoropolymer, achieving 5,000+ hours of ASTM B117 salt spray endurance.
Why Leading Engineers Choose Neelkamal Alloys LLP
As a global leader in high-integrity fastener manufacturing and export, Neelkamal Alloys LLP brings unmatched engineering expertise, state-of-the-art cold/hot forging technologies, and direct logistics networks servicing Malaysian ports:
End-to-End Traceability
Every batch of OEM hot galvanized fasteners is stamped with unique heat numbers, supported by EN 10204 3.1 material test certificates documenting mechanical yield, tensile strength, elongation, and Charpy impact values.
Custom Drawing Machining
Equipped with advanced multi-axis CNC turning and thread-rolling machinery, we produce non-standard pitch, extended shank lengths, shoulder studs, and special drawing-based OEM fasteners to exact buyer blueprints.
Comprehensive QA Testing
In-house quality control includes SPECTRO chemical analysis, magnetic particle inspection (MPI), ultrasonic flaw detection, coating thickness micro-gauging, and digital optical profile verification.
Direct Export Logistics
Dedicated freight routing directly from our Mumbai manufacturing hub to major Malaysian ports including Port Klang, Pasir Gudang, Penang Port, and Bintulu with complete customs documentation support.
Frequently Asked Questions (FAQ) - Procurement & Technical Specs
Direct answers for purchasing managers, structural engineers, and project contractors sourcing OEM fasteners for Malaysian projects:
What is the minimum coating thickness for your OEM hot-dip galvanized fasteners?
Our HDG fasteners strictly comply with ISO 1461, ASTM A153 (Class C for bolts over 3/8" and Class D for smaller sizes), and BS 729. The standard coating thickness ranges between 55 microns and 85 microns, customizable up to 100+ microns for severe marine exposure (C5-M rating).
How do you prevent thread binding during installation of galvanized nuts and bolts?
Zinc coating creates dimensional buildup on thread flanks. To ensure free-running assembly without thread stripping, we manufacture internal hex nuts overtapped to ISO 965-5 (6AZ or 6G tolerance) or ASTM A563 standards. This guarantees perfect thread engagement after hot-dip galvanizing without requiring re-tapping on site which would remove protective zinc.
Can you manufacture custom non-standard sizes based on engineering drawings?
Yes. We specialize in custom OEM manufacturing. Whether your project requires oversized anchor bolts up to M100 / 4" diameter, custom double-end studs, fine pitch threads, or special head geometry (dome, square weld, socket cap), our CNC machining division manufactures strictly to customer CAD/PDF drawings.
Are your fasteners certified for high-tensile structural applications?
Absolutley. We produce high-tensile structural bolts across Property Classes 8.8, 10.9, and 12.9, as well as ASTM A193 Grade B7/B7M, ASTM A325, and ASTM A490. All high-tensile bolts undergo post-pickling thermal stress relief baking at 200°C to eliminate any risk of Hydrogen Embrittlement.
What are the ocean freight lead times to Malaysia (Port Klang / Pasir Gudang)?
Standard manufacturing lead time for custom OEM orders ranges between 10 to 20 days depending on volume and specs. Direct sea freight transit from Mumbai Port to Port Klang or Pasir Gudang typically takes 7 to 12 days, allowing fast turnaround for urgent project schedules.
Do you provide Third-Party Inspection (TPI) and EN 10204 3.1 Mill Certificates?
Yes. Every shipment includes comprehensive EN 10204 3.1 Mill Test Certificates detailing raw material melt heat numbers, chemical breakdown, mechanical testing, and galvanizing thickness reports. We routinely accommodate Third-Party Inspection (TPI) agencies such as SGS, TÜV, Bureau Veritas, and Lloyd's Register upon request.
Ready to Secure High-Performance Galvanized Fasteners for Your Project?
Send us your bill of materials, engineering drawings, or quantity specifications. Our engineering sales experts provide immediate technical consultation, competitive wholesale quotes, and guaranteed fast delivery lead times.
Inquire Now