
Precision OEM/ODM Fastener Selection
Heavy-duty, hot-dip galvanized, stainless steel, and high-temperature alloy fasteners manufactured to ASTM, ASME, DIN, and ISO standards for rigorous engineering applications.
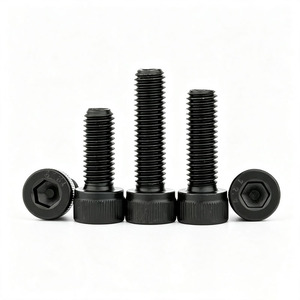
12.9 Grade Hardened Hex Socket Cap Head Screws Full Thread & Half Thread Available Screws
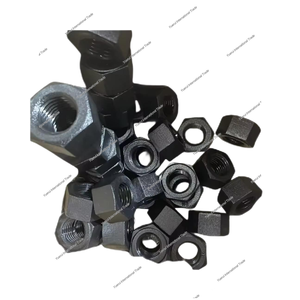
Custom Wholesale DIN934 Stainless Steel Heavy Hex Nut Factory Quality Factory Price Carbon Steel Galvanized Nuts
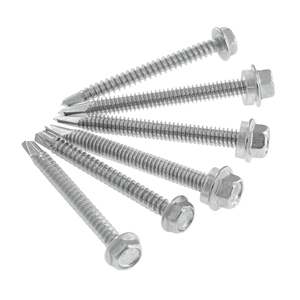
Direct Wholesale SS304 Stainless Steel Hex Flange Head Self Drilling Screw
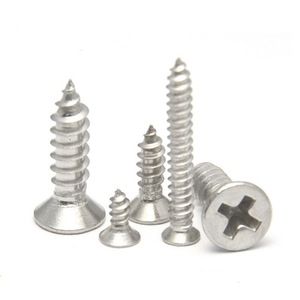
KA Countersunk Self-tapping Screws Hardened Carbon Steel Zinc Plated Phillips Cross Recessed OEM Customized
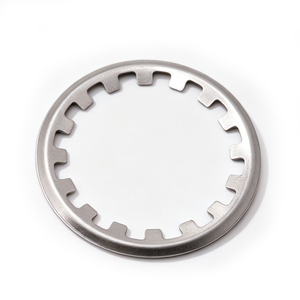
Custom Stainless Steel Internal Tooth Lock Washer Star Washer for Bolt Fastener Fixing
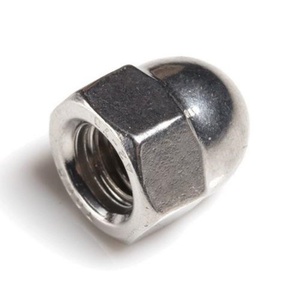
Customizable Incoloy825 Nickel Alloy Hex Nut With 10 Level Strength And High Temperature Resistance For Mechanical Equipment
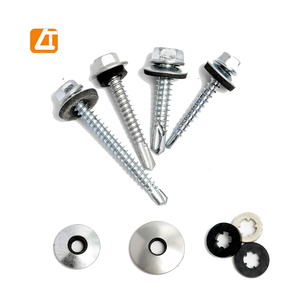
DIN7504K Tornillos Autoperforantes Hexagonal Self Drilling Screw Sizes Hex Head Roofing Screws with EPDM Bonded Rubber Washer
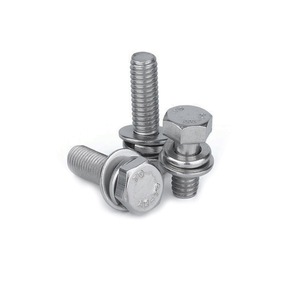
OEM Inconel 600/601/625/718 Combination Bolts and Nuts China Bolts with Nut DIN Standard
Hot-Dip Galvanized Fasteners in Chicago: Metallurgical Integrity in Severe Microclimates
The Chicago metropolitan area—encompassing Cook County, the Will County industrial corridor, and the surrounding Lake Michigan shoreline—presents one of North America's most demanding environmental operating conditions for structural steel fasteners. Industrial infrastructure in Chicagoland faces a punishing combination of relentless freeze-thaw cycles, high airborne humidity from Lake Michigan, industrial airborne pollutants, and heavy seasonal applications of deicing chemicals (sodium chloride, calcium chloride, and magnesium chloride). Standard electro-galvanized or zinc-plated fasteners rapidly succumb to red rust under these severe atmospheric exposures, compromising joint integrity and necessitating premature structural rehabilitation.
As premier OEM/ODM Hot Galvanized Fasteners Manufacturers & Suppliers serving the Chicago market, Neelkamal Alloys LLP engineers specialized metallurgical fasteners designed for maximum corrosion resistance and structural shear strength. Hot-dip galvanizing (HDG) as per ASTM A153/A153M and ASTM F2329 standards creates a series of zinc-iron alloy layers that form a metallurgical bond far superior to mechanical plating or thin electro-deposited zinc coatings.
The Metallurgy of Hot-Dip Galvanizing (HDG) Layering
During our controlled hot-dip galvanizing process, pre-cleaned high-tensile carbon steel and alloy fasteners are immersed in a molten zinc bath maintained at approximately 815°F to 850°F (435°C to 455°C). This process initiates a metallurgical reaction between the iron in the substrate steel and the molten zinc, forming four distinct microstructural phases:
Eta (η) Outer Layer
100% pure Zinc (Zn) outer shell providing immediate barrier protection and cathodic sacrifice. Soft and ductile to absorb impact during field installation.
Zeta (ζ) Layer
Monoclinic FeZn13 crystal structure containing 94% Zn and 6% Fe. Harder than the base carbon steel, providing exceptional abrasion resistance.
Delta (δ) Layer
Hexagonal FeZn10 structure (90% Zn, 10% Fe). Delivers remarkable mechanical bonding to structural steel and withstands micro-vibrations.
Gamma (γ) Layer
Cubic Fe3Zn10 inner layer (75% Zn, 25% Fe) fused directly into the steel matrix, ensuring zero coating delamination even under heavy thermal contraction.
This multi-layered sacrificial protection ensures that even if the outer surface is gouged during structural erection on site in Chicago, the surrounding zinc sacrifices itself electrochemically to protect the underlying steel substrate. This guarantees a service life exceeding 50+ years without maintenance in C3 to C4 industrial-coastal environments.
Chicago Market Engineering Specification Matrix
Comprehensive technical breakdown of fastener grades, thread clearances, surface treatments, and international compliance standards supported for OEM/ODM orders.
| Fastener Category | Material Grade Options | Dimensional Standards | Galvanizing / Coating Spec | Chicago Industry Application |
|---|---|---|---|---|
| Heavy Hex Structural Bolts | ASTM A325, ASTM A490, Grade 8.8, Grade 10.9, Grade 12.9 | ASME B18.2.1, DIN 931 / DIN 933, ISO 4014 | ASTM A153 Class C / ASTM F2329 (Hot-Dip Galvanized) | Bridges, Highway Girders (IDOT), High-Rise Steel Framing |
| Heavy Hex Nuts | ASTM A194 Gr 2H, Gr 8, Gr 8M, DIN 934, Carbon Steel Class 8/10 | ASME B18.2.2, DIN 934, ISO 4032 | Hot-Dip Galvanized with Over-tapped Threads (2B/3B fit) | Structural Joint Bolting, Flange Connections, Heavy Machinery |
| High-Tensile Socket Screws | Class 12.9 Alloy Steel, Hardened Carbon Steel, SS304 / SS316 | DIN 912, ISO 4762, ASME B18.3 | HDG / Mechanical Zinc / Thermal Diffusion Coating | Precision Automotive Assemblies, Heavy Manufacturing Equipment |
| Exotic Alloy Fasteners | Inconel 600/625/718, Incoloy 825, Hastelloy C276, Monel 400 | ASTM B166, B446, B637, Custom OEM Drawings | Passivated / Specialized Barrier / Native Oxide Protection | Petrochemical Refineries, Chemical Processing along Lake Michigan |
| Roofing & Self-Drilling Screws | Hardened Carbon Steel, Stainless Steel 304 / 316 | DIN 7504K, ASME B18.6.4 | Zinc Hot-Dip / EPDM Bonded Washer Assemblies | Commercial Logistics Warehouses, Cold Storage Facilities |
| Washers & Locking Fasteners | Carbon Steel, Stainless Steel (304, 316), Spring Steel | DIN 125, DIN 9021, Custom Tooth Lock Star Washers | ASTM F844, Hot-Dip Galvanized, Passivated | Railway Infrastructure, CTA Track Systems, Substation Grid |
Localized Applications Across Chicagoland Infrastructure
Empowering Chicago's vital economic sectors with field-tested, heavy-duty hot-galvanized structural fasteners.
Transportation & Highway Bridges (IDOT)
Chicago is North America's premier freight hub. Our hot-dip galvanized ASTM A325 and A490 structural bolts are extensively utilized in highway bridge retrofits along the Kennedy and Dan Ryan Expressways, offering superior resistance against heavy salt spray during winter deicing.
High-Rise Commercial Construction
From Downtown Chicago’s Loop to West Loop skyscrapers, our OEM/ODM custom structural fasteners secure curtain wall brackets, steel framing trusses, and elevator shaft assemblies where wind load stress and structural movement demand absolute fatigue endurance.
Port Facilities & Lake Michigan Marine Work
At the Port of Chicago and surrounding Lake Michigan maritime facilities, constant water exposure accelerates galvanic corrosion. Our HDG, SS316, and Incoloy 825 nuts and bolts maintain mechanical torque integrity in submerged and splash-zone structural joints.
Logistics & Cold Storage Distribution Hubs
With massive fulfillment centers expanding around O'Hare and Midway corridors, our self-drilling DIN 7504K roofing screws with bonded EPDM washers deliver leak-proof thermal expansion jointing for metal roofing and refrigerated storage envelopes.
Emerging Procurement Trends in Chicagoland's Industrial Sector
The industrial fastener landscape across Illinois and the broader Midwest is shifting rapidly due to stricter municipal building codes, sustainable construction mandates, and supply chain localization requirements. Fastener procurement managers in Chicago are increasingly focusing on three pivotal trends:
1. Transition to Eco-Friendly Hot-Dip Galvanizing & Zero-Chromate Passivation
In response to Midwest environmental standards and LEED certification criteria for modern commercial developments, OEMs are specifying hot-dip galvanizing facilities that employ lead-free zinc kettles and zero-hexavalent-chromium passivation. Our manufacturing lines adhere strictly to eco-compliant galvanizing practices, reducing environmental footprint while boosting salt spray corrosion endurance beyond 1,000 hours.
2. Precision Thread Engineering for Post-Galvanizing Fitment
A classic bottleneck in heavy construction is thread binding or galling when standard nuts are paired with hot-dip galvanized bolts. Because HDG adds a coating thickness ranging from 45 to 100 microns (1.8 to 4.0 mils), threads must be engineered with explicit pitch overtapping. As specialized OEM manufacturers, we custom-tap female threads on DIN934 and ASME B18.2.2 Heavy Hex Nuts post-galvanizing, guaranteeing smooth hand-assembly on site while maintaining standard proof-load ratings.
3. Demand for High-Temperature Exotic Alloys in Midwest Processing Plants
Beyond standard HDG carbon steel, Chicago’s vast industrial belt (including petroleum refining, power generation, and chemical manufacturing) requires specialty alloys capable of operating under high pressure and aggressive chemical exposure. Neelkamal Alloys LLP fulfills this niche by stocking and manufacturing custom Inconel 600/625/718, Incoloy 825, Hastelloy C276, and Titanium Grade 2/5 fasteners that withstand temperatures up to 1800°F (982°C) without oxidation or creep failure.
Neelkamal Alloys LLP: Global Manufacturing Excellence Served to Chicago
As an ISO certified manufacturer, stockist, and exporter, Neelkamal Alloys LLP brings extensive metallurgical expertise to structural engineers, EPC contractors, and industrial procurement teams throughout Chicago. Every order is executed with full heat-number material traceability, rigorous dimensional inspection, and certified mechanical testing.
EN 10204 3.1 Certification
Complete Mill Test Reports provided with every shipment detailing chemical composition, yield strength, tensile strength, and elongation.
Custom OEM/ODM Manufacturing
Precision machining and cold/hot forging tailored to complex engineering drawings, custom head geometries, and special thread profiles.
Rigorous Quality Assurance
In-house PMI testing, hardness testing (Rockwell/Vickers), salt spray chamber testing (ASTM B117), and third-party inspection (TUV, SGS, BV).
Seamless Logistics to Chicago
Seaworthy export packaging, palletized bundle protection, and rapid customs documentation for fast delivery to Midwest job sites.
Frequently Asked Questions by Chicago Buyers
Expert engineering answers to common technical queries regarding HDG fasteners, standards compliance, and custom ordering.
What is the difference between Hot-Dip Galvanizing (HDG) and standard Zinc Plating for Chicago structural applications?
Standard zinc electroplating (ASTM B633) deposits a thin layer of zinc (typically 5 to 25 microns) offering minimal barrier protection suited mainly for indoor applications. In contrast, Hot-Dip Galvanizing (ASTM A153 / F2329) immerses the steel in molten zinc, creating a thick (45 to 100+ microns) metallurgically bonded zinc-iron alloy coating. For Chicago's outdoor infrastructure exposed to deicing salts and freeze-thaw cycles, HDG is essential to prevent red rust corrosion for decades.
How do you ensure HDG heavy hex nuts fit smoothly on galvanized bolts without thread locking?
Due to the coating thickness of hot-dip galvanizing, standard male and female threads will bind if assembled without allowance. We resolve this by over-tapping female nut threads post-galvanizing (or pre-galvanizing with controlled clearance) as per ASTM A563 / ASME B18.2.2 specifications. This ensures optimal 2B/3B thread fit while maintaining full tensile and proof load ratings.
Can Neelkamal Alloys LLP manufacture custom fasteners based on CAD drawings?
Yes. As a full-service OEM/ODM manufacturer, we produce custom-machined and forged fasteners based on customer-supplied CAD drawings or PDF specifications. Whether you require non-standard shank lengths, special step-down diameters, unusual head profiles, or custom pitch threads, our CNC machining facilities deliver precise tolerances.
How do you prevent Hydrogen Embrittlement in high-strength 12.9 grade galvanized fasteners?
High-strength steels with tensile strength exceeding 1000 MPa (such as 12.9 grade fasteners) are vulnerable to hydrogen embrittlement during acid pickling prior to galvanizing. We mitigate this risk by employing mechanical descaling or baking the fasteners at controlled temperatures (around 190°C to 210°C) immediately after acid cleaning to de-gas absorbed hydrogen prior to hot-dip zinc immersion.
What documentation accompanies export orders delivered to Chicago buyers?
All export orders from Neelkamal Alloys LLP include comprehensive documentation: Material Test Certificates (MTC) per EN 10204 3.1, Chemical Analysis Reports, Mechanical Test Results (Yield, Tensile, Hardness, Impact), Galvanizing Coating Thickness Certificates, Commercial Invoices, Packing Lists, and Certificates of Origin.
What is the typical lead time for custom OEM fastener delivery to Chicago?
Standard stocked items can be packed and dispatched within 3 to 7 business days. Custom OEM/ODM production runs typically take 2 to 4 weeks depending on order volume and material specifications. We coordinate expedited air freight or sea freight directly to Chicago ports and distribution centers to align with your project timelines.